From carefully sourced Non-Basmati Raw Rice to our upcoming Premium Packaged Drinking Water, we are committed to delivering products that reflect purity, consistency, and trust. Backed by modern milling technology, stringent quality standards, and a customer-first approach, we proudly serve domestic and global markets with excellence.
For generations, we have been committed to delivering premium-quality rice through modern milling processes and uncompromising quality standards. Every grain is carefully selected, processed, and packaged to preserve its natural freshness, purity, and nutritional value. By combining advanced technology with responsible sourcing, we ensure consistency that meets the expectations of distributors, retailers, and consumers alike.
Our focus extends beyond production, we believe in building lasting relationships through reliability, transparency, and excellence. With an extensive range of rice varieties and a dedication to continuous improvement, we strive to support households, businesses, and global markets with products that reflect quality, trust, and sustainable growth.
Explore our wide range of high-quality non-basmati rice varieties, carefully processed to meet the diverse needs of households, businesses, and global markets.
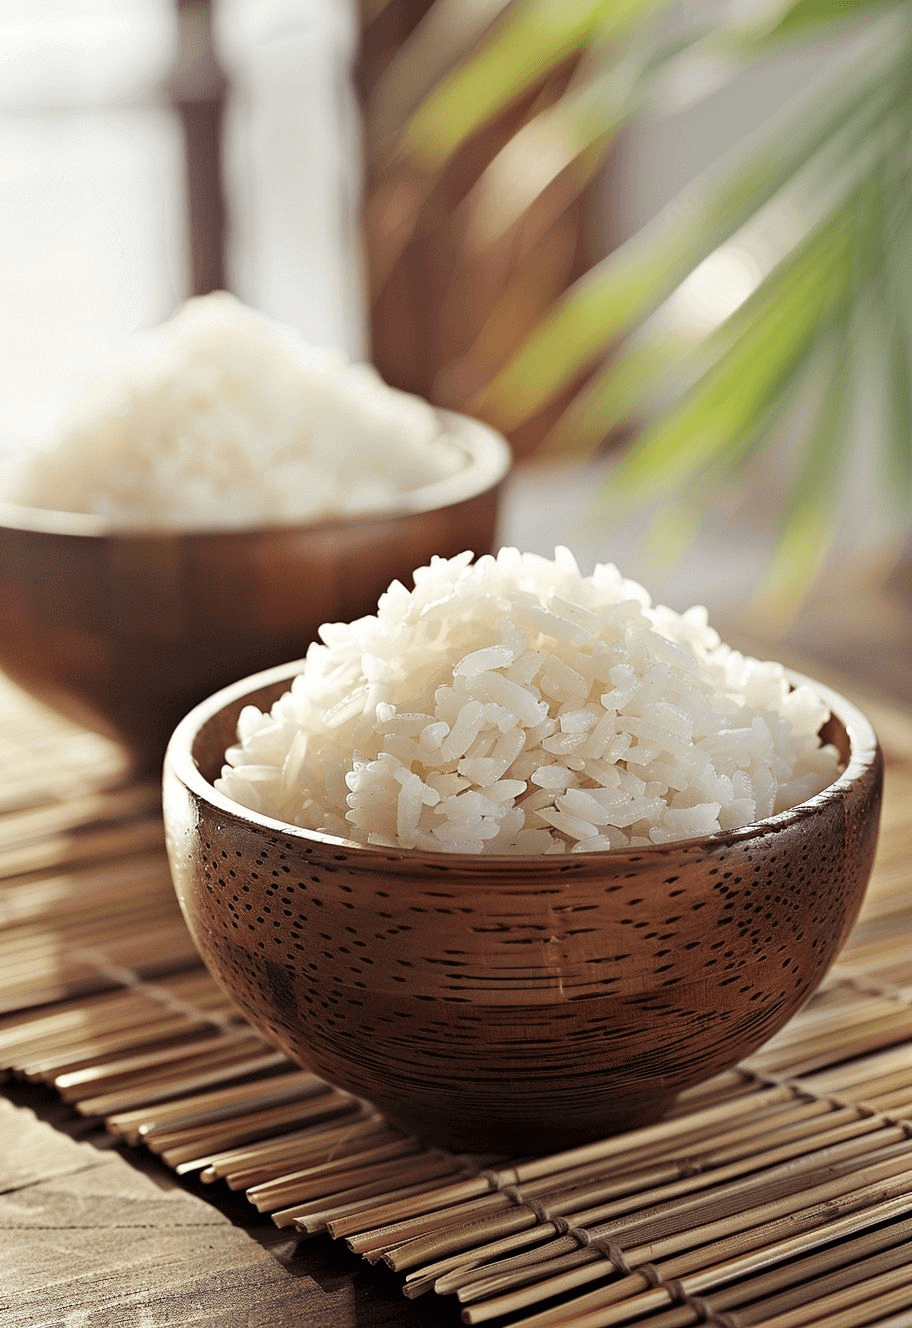
Lightweight, aromatic, and easy to digest with a soft texture after cooking.
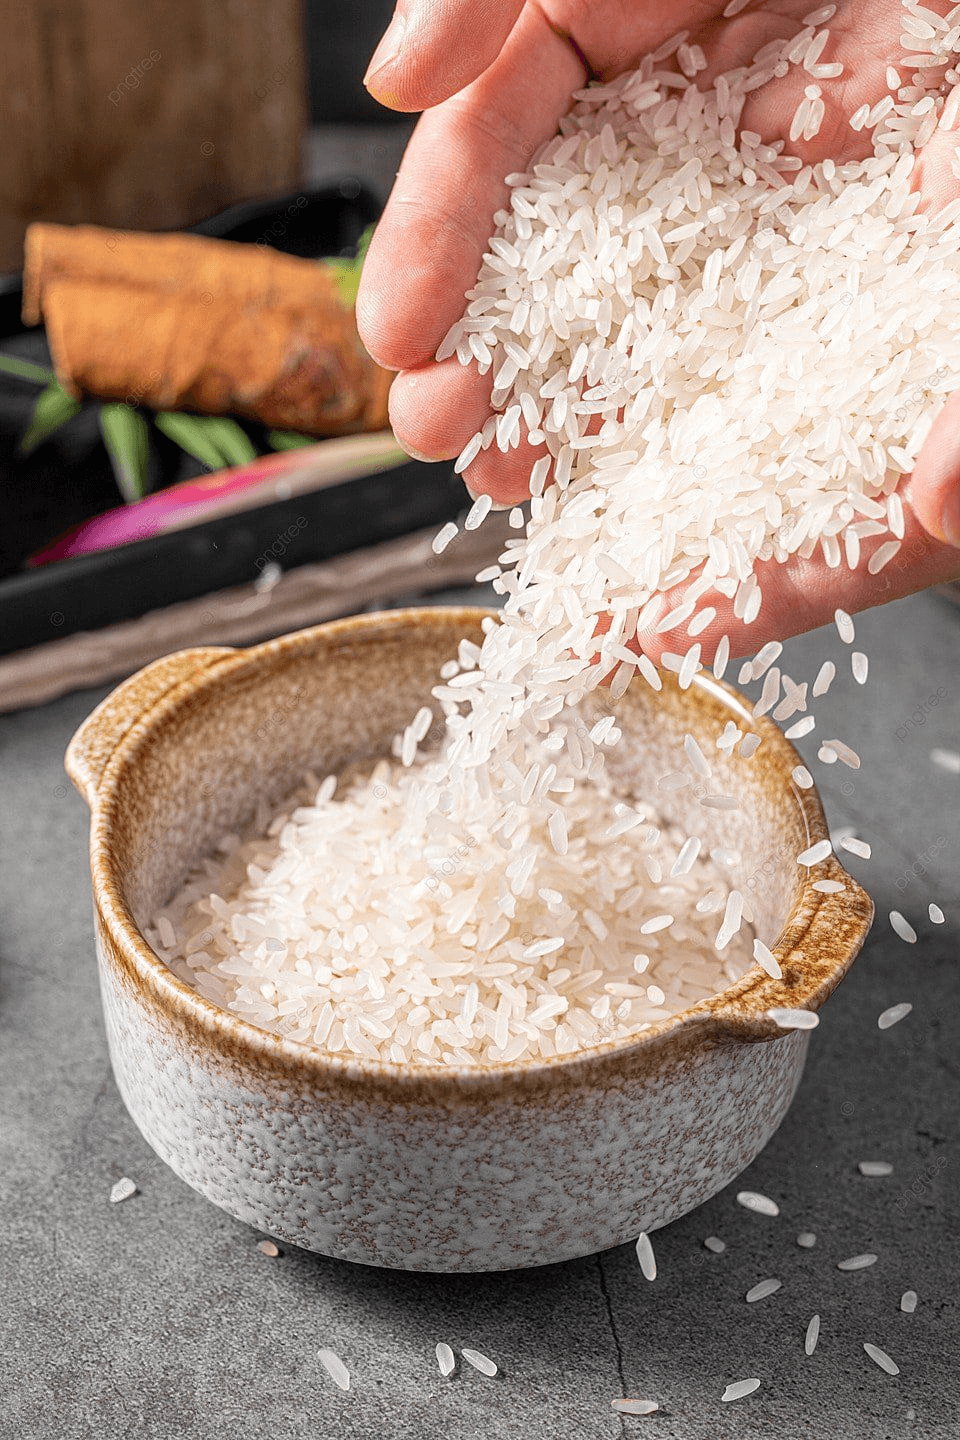
Lightweight, aromatic, and easy to digest with a soft texture after cooking.
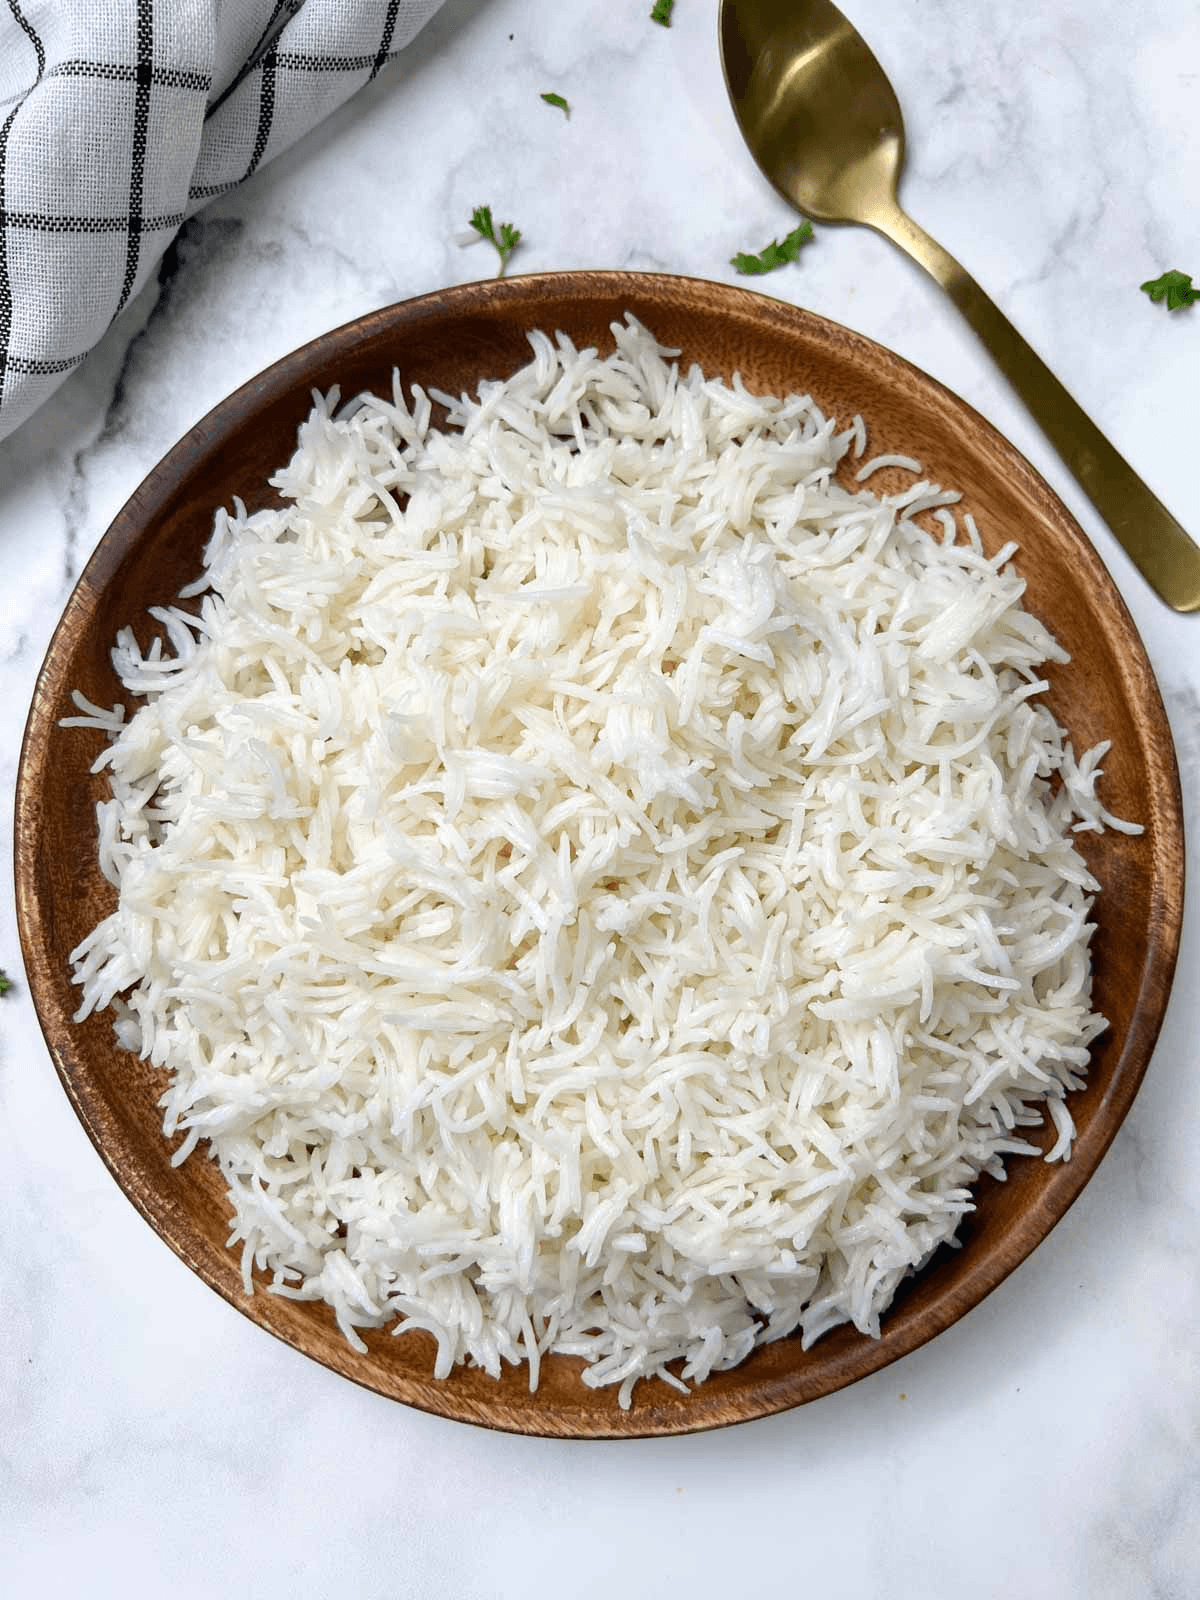
Lightweight, aromatic, and easy to digest with a soft texture after cooking.
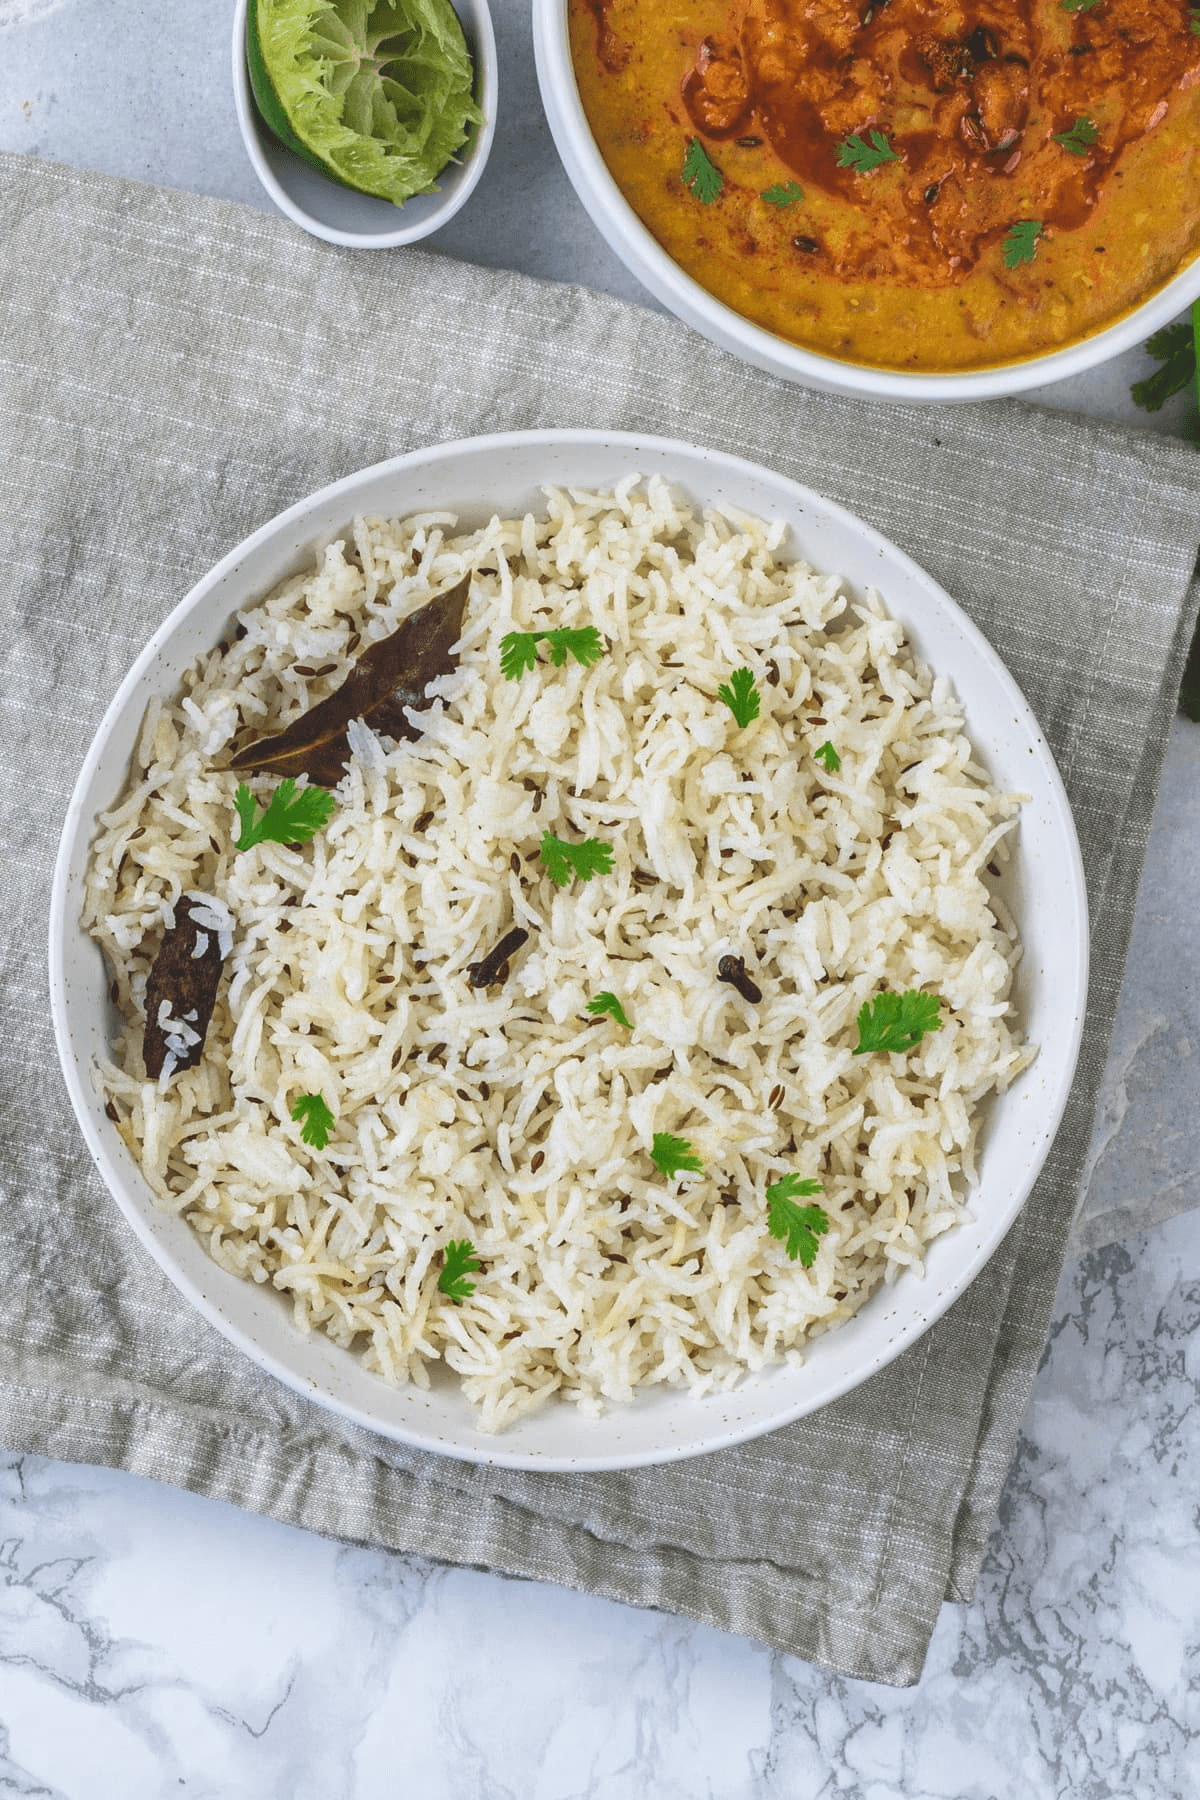
Lightweight, aromatic, and easy to digest with a soft texture after cooking.
Explore our wide range of high-quality non-basmati rice varieties, carefully processed to meet the diverse needs of households, businesses, and global markets.
Every certification represents our dedication to delivering products that meet recognized national and international quality benchmarks. From sourcing premium grains to hygienic processing and secure packaging, every stage is monitored to ensure excellence and reliability.
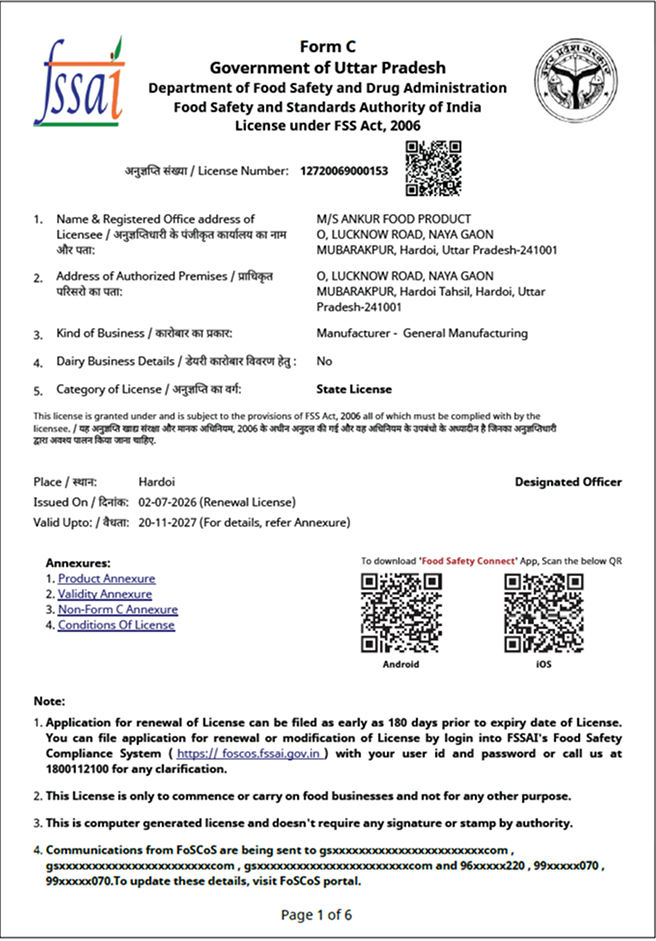
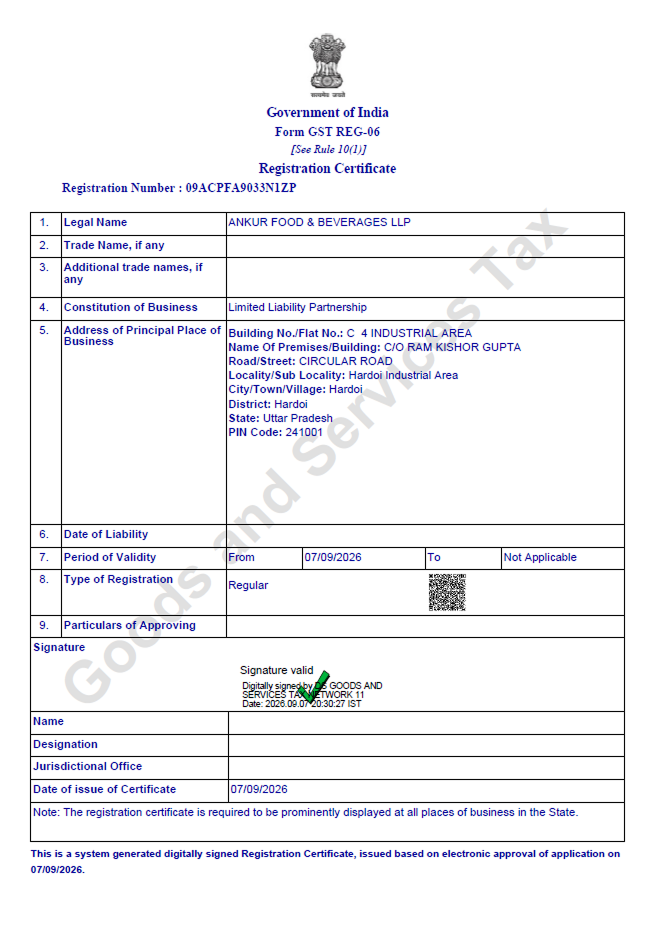
We follow a carefully monitored milling process that combines advanced technology with strict quality control to deliver clean, nutritious, and great-tasting rice.
Procuring premium-quality paddy from mandis, inspecting every batch upon arrival at the factory, and storing it under ideal conditions for further processing.
Removing dust, stones, straw, metal fragments, and other impurities with advanced cleaning equipment to ensure consistent grain quality before milling.
Removing the protective outer husk from the paddy using precision milling equipment while preserving the quality of the rice kernels.
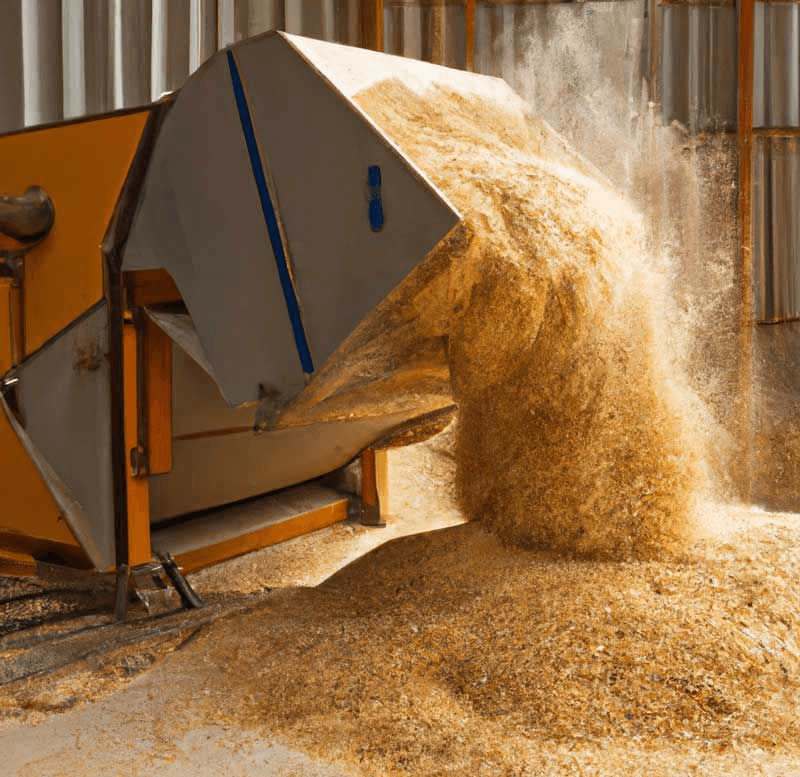
Separating unhusked paddy from brown rice using gravity-based technology, returning remaining paddy for dehusking while forwarding brown rice.
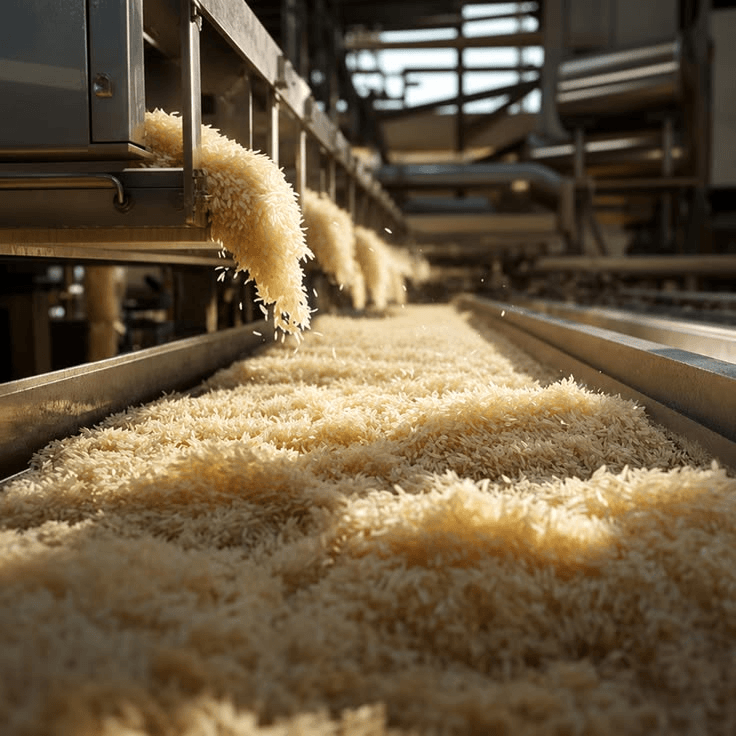
Removing the outer bran layer with advanced whiteners and silky polishers to produce smooth, shiny, and premium-quality white rice.
Using advanced color sorters to identify and remove discolored, damaged, or defective kernels, ensuring a uniform and premium-quality rice output.
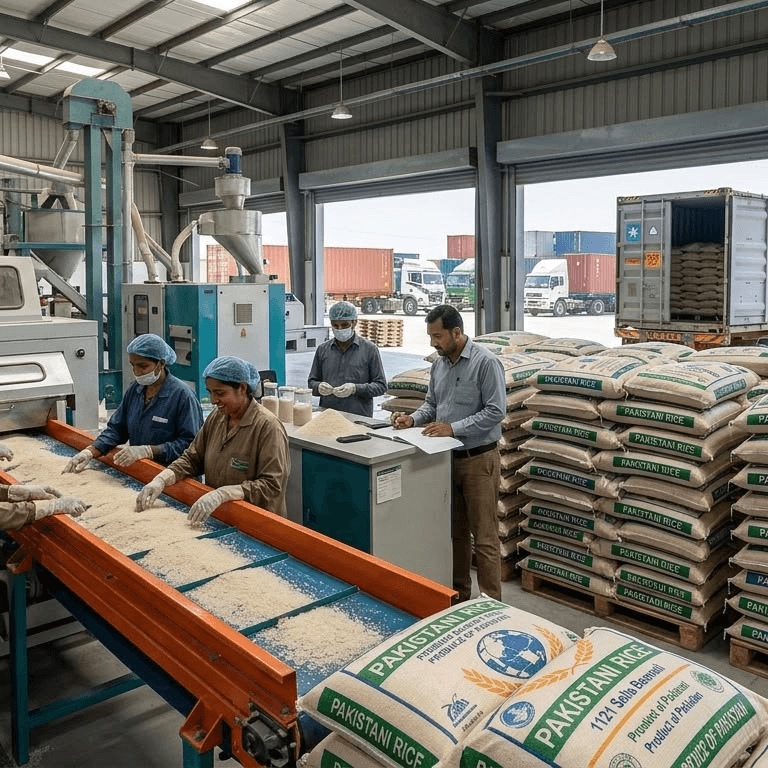
Separating broken grains and grading rice by kernel length using precision grading machines to achieve consistent size and superior quality.
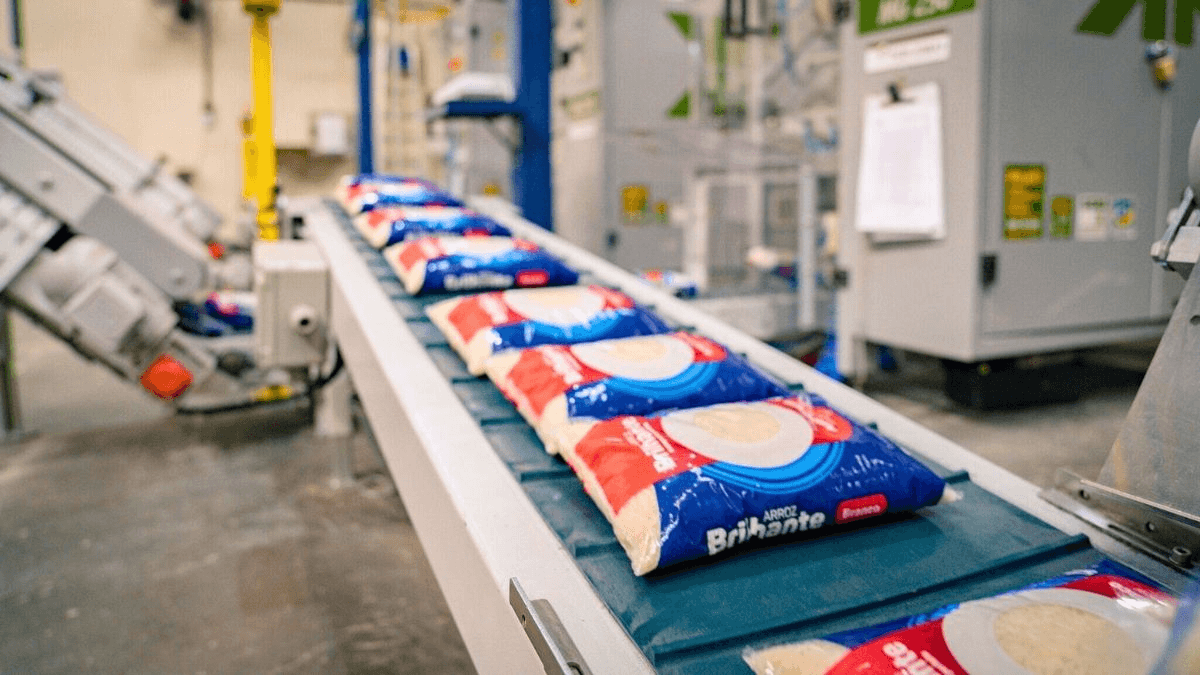
Packaging the finished rice in durable, food-grade bags to preserve freshness, maintain quality, and ensure safe distribution to customers.